
Wheat Flour Machinery Plant Essentials for Efficient Flour Production
2026-10-16
If you're planning or upgrading a wheat flour machinery plant, efficiency isn't just a buzzword—it's the margin between profit and loss. The right layout, robust cleaning systems, precise milling units, and smart sifting technology all work together to turn raw wheat into consistent, high-quality flour. PINGLE has built turnkey flour plants for decades, knowing exactly where bottlenecks hide and how to eliminate them. In this blog, we'll walk you through the essential components that make a flour mill run smoothly and efficiently—so you can avoid costly trial and error.
Start with Grain That Arrives Ready to Work
Opening a bag shouldn’t feel like a gamble. Every lot is screened, aspirated, and size-graded before it ever reaches your dock, so you’re not paying for chaff, stones, or surprises. The moisture level is already dialed in, and the kernel count per gram stays within a tight band — which means your mash, dough, or mill stream behaves the same from the first scoop to the last.
That consistency shows up where it counts. You can skip the pre-cleaning step, shorten your setup time, and trust that the starch or protein profile won’t drift mid-run. It’s grain that respects your schedule and your recipe, not a raw material that needs constant babysitting.
Cleaning Steps That Protect Your Core Equipment
Before touching any core equipment, cut the power and let capacitors discharge for at least ten minutes. This step sounds obvious, but plenty of failures trace back to a rushed wipe-down while the machine still held residual charge. Ground yourself with a wrist strap, and keep the room humidity above 40% to reduce static buildup. Then pull out the manual or the maintenance log to see which enclosures can be opened and which seals should never be broken.
Use a soft-bristle brush or a low-pressure air blower (under 30 PSI) to remove dust from vents, heat sinks, and fan blades. Do not let the fans spin freely while blowing air through them — hold each blade still with a toothpick or a non-conductive tool, otherwise you risk generating back-current that can damage the controller board. For sticky residue on metal housings, dampen a lint-free cloth with isopropyl alcohol and wipe along the grain, never in circles. Avoid spraying any liquid directly onto connectors or gaskets.
After cleaning, wait until all surfaces are completely dry before reconnecting power. Inspect cable routing for pinched wires or loose clips, and run a short self-test or boot sequence while watching for unusual noise or temperature spikes. Write down what you cleaned and any parts that looked worn, so the next maintenance window starts with useful history instead of guesswork.
Conditioning for a Steadier Milling Run
A steadier milling run often starts well before the cutter meets the workpiece. Let the spindle come up to speed and run at a moderate RPM for a short warm-up cycle, so bearings and tool holder settle into their usual thermal state. If coolant is part of your setup, give it time to reach a consistent temperature rather than flooding a cold tool and shock-loading the edge. These small pauses prevent the slow drift in dimensions that shows up halfway through a batch.
Pay attention to the material too. Stock that has been sitting in a cold warehouse or near a heat source can move once you start removing metal, so bring it into the shop environment and let it rest before clamping. Check that the workholding is evenly torqued and that there is no trapped swarf under the parallels. A few minutes spent on these conditioning steps usually means fewer surprises in surface finish, less chatter, and a run that holds size from first part to last.
The Right Roll Configurations for Each Flour Fraction
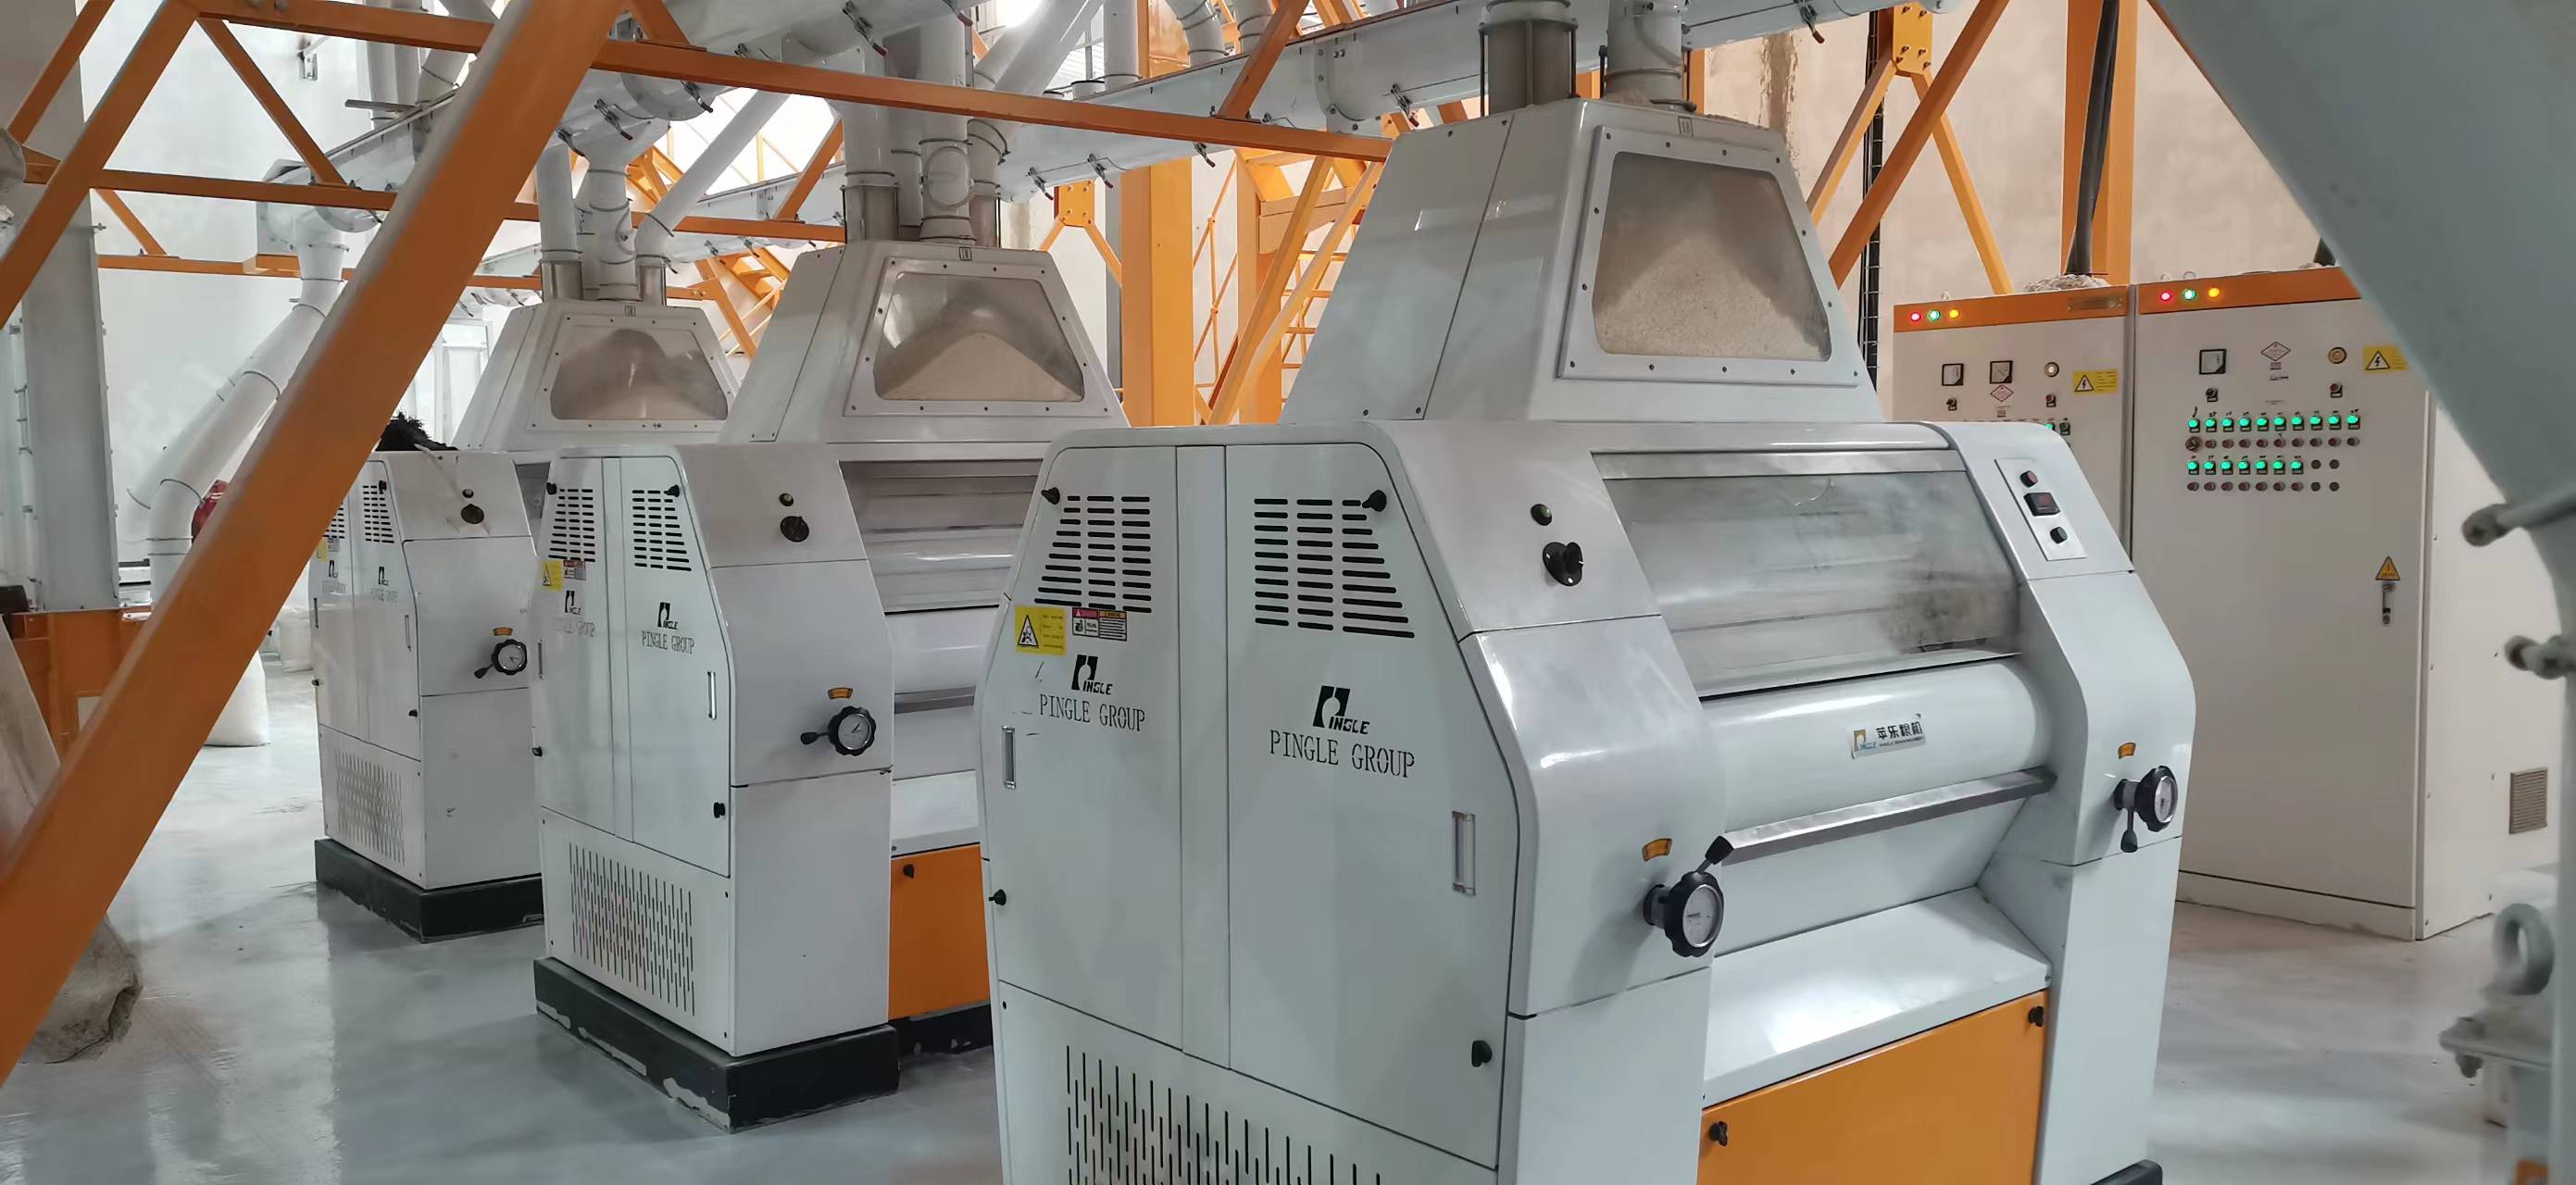
Break rolls handling the first three passages need deeper corrugations and aggressive differential speeds, usually around 2.5:1, to peel bran away from endosperm without shattering the outer layers. Once you move to sizing and middlings reduction, the profile flattens out; finer corrugations or smooth rolls with a 1.25:1 differential do a cleaner job of reducing clean semolina into flour without overheating the stock.
For tail-end passages where bran and germ fragments are still present, a light grind with just enough shear keeps those particles from breaking down into ash. Many mills run smooth rolls at low differential here, sometimes under 1.1:1, and rely on roll gap rather than speed to do the work. The payoff shows up in lower ash and a brighter flour colour from the later reduction stages.
Fraction-specific settings also matter for moisture and feed rate. A coarse middlings fraction accepts a tighter gap and faster feed, while fine semolina needs a slightly wider gap and lower differential to avoid creating excess starch damage. Adjusting these roll parameters per fraction is what separates a balanced mill balance from one that fights flour quality every shift.
Sifting and Purification Without Letting Good Material Slip
A lot of separation processes fail quietly: the purity numbers look fine, but the reject stream carries away material that should have stayed. Sifting works best when the screen openings, feed consistency, and vibration are matched to the actual particle range, not to a generic spec. If the angle is too steep or the material too dry, fines bounce off instead of passing through, and good product ends up in the discard pile.
Purification needs the same attention at every step. Rather than relying on a single aggressive cut, it helps to use a staged approach—first remove the obvious contaminants, then refine the remaining stream with gentler methods. Watching the tailings closely tells you more than the accepted output ever will. When recoverable material starts showing up there, a small adjustment in air flow, wash pressure, or screen mesh can bring it back into the product line without compromising purity.
The practical habit is to sample both streams at fixed intervals and compare what’s leaving against what’s being kept. That comparison often exposes a simple fix: a worn screen, a misaligned chute, or a feed rate that pushes too much material across too little area. Fixing those issues returns lost yield without adding new equipment. Good separation isn’t about catching everything at once—it’s about keeping the valuable fraction in the circuit until only true waste remains.
Packing and Storage Built for Daily Output
The packaging system is designed with a single goal in mind: keeping up with the pace of daily output without slowing down your team. Each container uses a modular tray layout that lets you stack, label, and grab individual parts without unboxing the entire supply. The outer shells are made from high-density corrugated board with a water-resistant coating, so they can sit near production lines or in delivery bays without degrading from minor spills or humidity.
Storage follows the same logic. Vertical shelving grooves along the side walls allow the packs to slide into place and lock with a simple push, eliminating the need for additional strapping or wrapping. Color-coded end caps tell you at a glance whether a box holds fasteners, electrical components, or finished subassemblies. Because the packs are uniform in width, they fit standard racks used in small-batch assembly cells and larger fulfillment centers alike.
Daily replenishment becomes less about hunting and more about reaching. The front-facing pull tabs are angled so you can extract a unit with one hand while holding a scanner in the other. Empty packs collapse flat to about a third of their assembled height, keeping return shipments cheap and storage aisles clear. This isn't packaging that sits forgotten in a back room—it moves with the rhythm of each shift.
FAQ
The core lineup usually includes a receiving and pre-cleaning section, tempering bins, roller mills, plansifters, purifiers, and pneumatic conveying systems. What separates a smooth-running plant from a bottleneck is how well these units are sized to match grain hardness and target extraction rates.
Focus on the grinding stages where most power is lost. Using corrugated rolls for breaking and smooth rolls for reduction, adjusting roll gaps precisely, and installing variable frequency drives on pneumatic fans often trims energy use by 10–20%. Good sifter balance also prevents over-grinding, which wastes both power and starch.
Tempering toughens the bran and softens the endosperm, so the roller mill can separate them cleanly. If moisture addition is inconsistent or rest time is too short, you either get bran flakes in the flour or low extraction. A well-managed tempering process directly improves milling yield and reduces wear on rolls.
Daily checks on roller bearings, sifter screens, and pneumatic airlocks catch most failures early. Scheduling roll re-fluting based on tonnes ground rather than calendar days prevents dull rolls from tearing bran. Keeping a log of vibration and temperature readings helps you replace parts before they break during a peak run.
Automation handles batching, moisture control, and roll gap adjustments with repeatability that manual operation cannot match. The real payoff is tighter control of extraction rate and ash content across shifts. Operators spend less time on guesswork and more time responding to alarms that indicate gradual drift.
Dust explosion prevention ranks first: proper grounding, magnetic separation before grinding, and explosion vents or suppression systems in filter housings. Beyond that, lockout/tagout procedures during roll maintenance and regular cleaning of confined spaces like bins and spouts are essential because flour dust is combustible and corners can hide smoldering material.
Sifter efficiency depends on the screen area, number of sections, and the sieve cleaning system. A plansifter with reliable sieve cleaning keeps mesh open longer and avoids flour carryover into semolina streams. Also look at drive stability because any vibration beyond specification reduces separation sharpness and creates uneven flour granulation.
Start by setting roll gaps and sifter clothing for the desired break release, then sample each stream every few hours. If ash creeps up, tightening the reduction rolls or cleaning purifier sieves usually brings it back. Remember that pushing extraction too high often pulls bran particles into the flour, so the target is the highest yield at stable ash, not the maximum theoretical yield.
Conclusion
A flour mill only runs as smoothly as the grain it receives, so the first decision is to work with wheat that has already been dried, sorted, and brought to a uniform moisture range before it ever reaches the intake pit. Once inside, the cleaning line does more than remove obvious field trash; it uses a sequence of magnets, rotary screens, destoners, and gentle scourers to pull out stones, ferrous fragments, and loose hulls that would otherwise chew through roll corrugations and sifter screens. Skipping a single cleaning stage rarely shows up in the first week, but it quietly shortens the life of every downstream machine.
Conditioning adds the missing piece: a day or two of rest after tempering lets moisture migrate into the endosperm, softening the bran and making the next roller pass steadier instead of brittle and dusty. From there, roll configurations need to be matched to what each fraction actually needs—break rolls should tear open kernels without shattering bran, while reduction rolls press middlings into flour with as little heat as possible. Sifting and purification then work as a pair; plansifters grade by particle size, and purifiers use small air currents to lift out light bran specks before good middlings are sent back to the rolls. Finally, packing and storage should not be left as an afterthought. A mill that fills bags, totes, or bulk bins without slowing the line keeps daily output moving and avoids the common bottleneck where finished flour waits on a slow scale or a poorly vented bin.
Contact Us
Contact Person: Jiakuo Wu
Email: [email protected]
Tel/WhatsApp: +86-13011566087
Website: https://www.pinglemachine.com